 VIPSolutions
Act like a helpful tutor and exlain me : Give step-by-step solution with explanation and final answer: do not include tables in your answer , solve first question only1. In a turning operation, the diameter of the work- piece is 2 inches (50 mm), and it rotates at 360 revolutions per minute. How long will a carbide tool last (n = 0.3) under such conditions if an identical carbide tool lasted for | minute when used at 1000 feet per minute (305.0 m/min.)? 2. When turning a thin tube at its edge, the follow- ing conditions were observed: Undeformed chip thickness 0.125 inch Chip thickness: 0.15 inch Back rake angle: 8° Cutting speed: 300 ft/min. Calculate the a. Cutting ratio b. Shear angle ¢. Chip velocity 3.. A geared-head lathe is employed for machining steel AISI 1055. BHN 250. The cutting speed is 400 feet per minute, and the rate of metal re- moval is 2.4 cubic inches per minute. If the tool used has the character 0-7-7-7-15-15-1/32, esti- mate the following: a. The energy consumed in machining per unit time b. The power required at the motor ¢. The tangential component of the cutting force Neglect the correction factor for the undeformed chip thickness.
Question:
Act like a helpful tutor and exlain me :
Give step-by-step solution with explanation and final answer:
do not include tables in your answer , solve first question only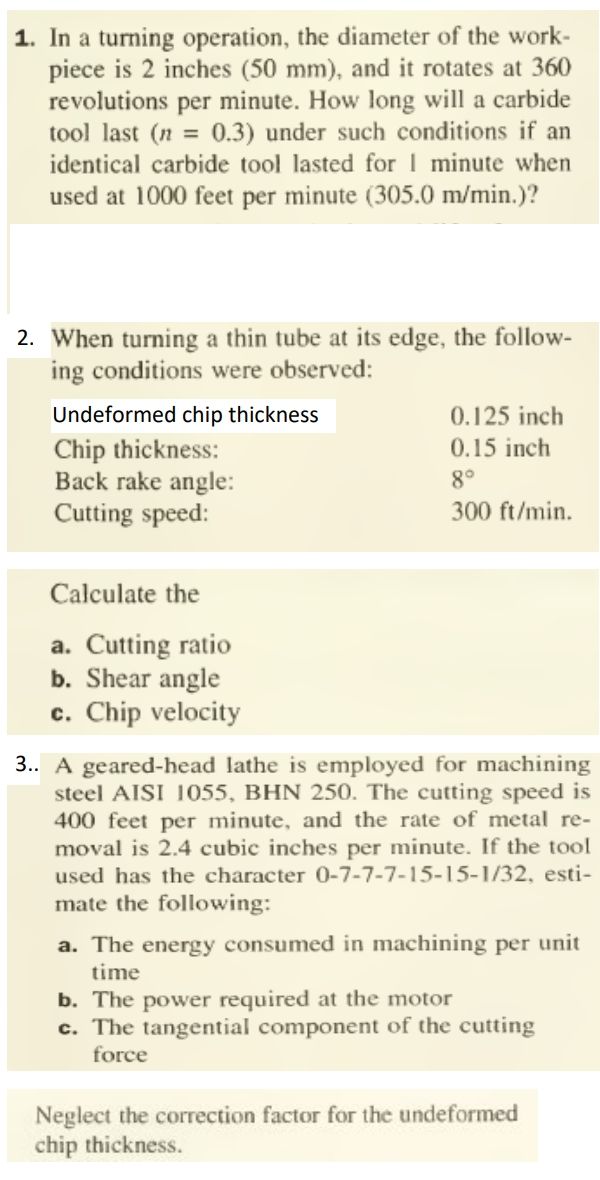 1. In a turning operation, the diameter of the work-
piece is 2 inches (50 mm), and it rotates at 360
revolutions per minute. How long will a carbide
tool last (n = 0.3) under such conditions if an
identical carbide tool lasted for | minute when
used at 1000 feet per minute (305.0 m/min.)?
2. When turning a thin tube at its edge, the follow-
ing conditions were observed:
Undeformed chip thickness 0.125 inch
Chip thickness: 0.15 inch
Back rake angle: 8°
Cutting speed: 300 ft/min.
Calculate the
a. Cutting ratio
b. Shear angle
¢. Chip velocity
3.. A geared-head lathe is employed for machining
steel AISI 1055. BHN 250. The cutting speed is
400 feet per minute, and the rate of metal re-
moval is 2.4 cubic inches per minute. If the tool
used has the character 0-7-7-7-15-15-1/32, esti-
mate the following:
a. The energy consumed in machining per unit
time
b. The power required at the motor
¢. The tangential component of the cutting
force
Neglect the correction factor for the undeformed
chip thickness.
Asked by: manish kumar
Created at: 2025-10-24 23:32:24
Final Answer:
📢 Instructions:
- Ask anything relatd to above question only.
- For new Question goto :